NMNH




Other Name:NMNH, β-Nicotinamide mononucleotide Reduced;Reduced β - nicotinamide mononucleotide; β-nicotinamide mononucleotide, reduced form, disodium salt(NMNH)
CAS NO.: 108347-85-9
Molecular Formula: C11H18N2NaO8P
Molecular Weight: 360.23
Active ingredients:β-nicotinamide mononucleotide, reduced form
Purity:Min98%
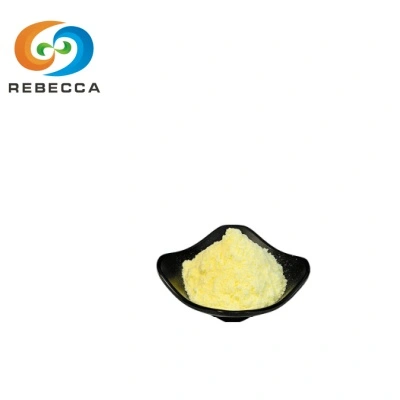
Appearance: Yellowish powder
Test Method: HPLC
MOQ: 1kg
Sample: 20g
Delivery: FedEx, DHL, Ship by air, Ship by sea.
Certifications: ISO, HACCP, KOSHER, HALAL
- Product Description
NMNH Raw Material | High-Purity NAD+ Precursor for Advanced Anti-Aging Solutions
NMNH, also known as Reduced β-Nicotinamide Mononucleotide Disodium Salt, is an innovative and upgraded cellular energy supplement raw material in the anti-aging ingredient industry. Different from traditional NAD+ precursors that rely on complex enzymatic conversion in the human body, this reduced-structure active molecule can directly boost intracellular NADH and NAD+ levels through efficient metabolic pathways. Verified by professional scientific researches, it delivers far higher bioavailability than conventional NAD+ raw materials under the same dosage, effectively solving the long-standing low absorption efficiency pain point of the industry. Shaanxi Rebecca Biotechnology specializes in supplying pharmaceutical-grade NMNH via mature green enzymatic synthesis technology. With zero heavy metal contamination and stable batch consistency, our product is the ideal high-quality raw material for manufacturers to develop premium anti-aging and longevity health products.
Technical Specifications
|
Parameter |
Specification |
||
|
Product Name |
Reduced β-Nicotinamide Mononucleotide Disodium Salt |
||
|
CAS Number |
108347-85-9 |
||
|
Molecular Formula |
C₁₁H₁₅N₂O₈PNa₂ |
||
|
Molecular Weight |
380.20 g/mol |
||
|
Appearance |
Off-white to pale yellow fine powder |
||
|
Purity (HPLC) |
≥98%, ≥99% |
||
|
Moisture Content |
≤5.0% |
||
|
Residue on Ignition |
≤15.0% |
||
|
Heavy Metals (Pb/As/Cd/Hg) |
≤0.5 ppm each |
||
|
Total Aerobic Bacteria |
≤100 CFU/g |
||
|
Yeast & Mold |
≤10 CFU/g |
||
|
Shelf Life |
24 months (proper storage) |
||
|
Storage Conditions |
Sealed, dry, dark, 2–8°C |
||
| Test Item | Specification | Test Result | Test Method |
|---|---|---|---|
| Appearance | White to off-white crystalline powder | Off-white crystalline powder | Visual inspection |
| Assay (NMNH) | ≥98.0% | 98.6% | HPLC |
| Related Substances (Single impurity) | ≤0.50% | 0.21% | HPLC |
| Total Impurities | ≤1.50% | 0.78% | HPLC |
| Loss on Drying | ≤2.0% | 0.84% | 105℃, 2h |
| Residue on Ignition | 18.0 ~22.0% | 19.6% | Gravimetric method |
| pH (1% aqueous solution) | 5.0 ~7.0 | 6.1 | pH Meter |
| Heavy Metals | ≤10 ppm | <10 ppm | AAS |
| Lead (Pb) | ≤3 ppm | <3 ppm | AAS |
| Arsenic (As) | ≤2 ppm | <2 ppm | AAS |
| Cadmium (Cd) | ≤1 ppm | <1 ppm | AAS |
| Mercury (Hg) | ≤0.1 ppm | <0.1 ppm | AAS |
| Total Aerobic Count | ≤1000 CFU/g | 132 CFU/g | GB 4789.2 |
| Yeast & Mold | ≤100 CFU/g | <10 CFU/g | GB 4789.15 |
| E‑coli | Negative | Negative | GB 4789.38 |
| Salmonella | Negative | Negative | GB 4789.4 |
Why Choose Us
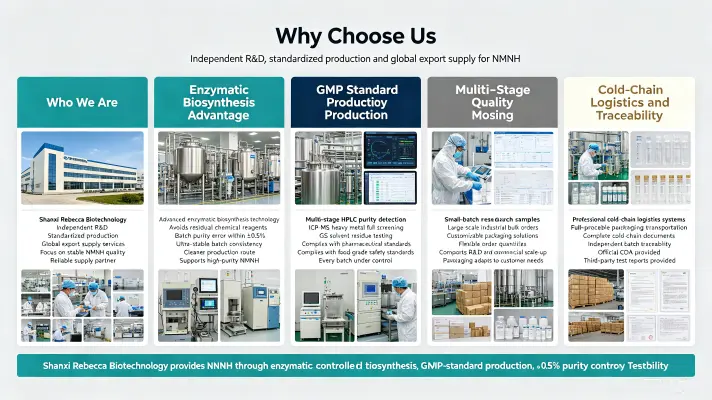
Shaanxi Rebecca Biotechnology integrates independent R&D, standardized production and global export supply services. We adopt advanced enzymatic biosynthesis technology and strict pharmaceutical-grade quality control systems to ensure stable product quality. Our unique enzymatic catalytic production process completely avoids residual chemical reagents, with the batch purity error strictly controlled within ±0.5%, realizing ultra-stable batch consistency.
We operate GMP-standard dust-free production workshops, with real-time monitoring and data recording of all key production parameters. Every batch of NMNH undergoes multi-stage HPLC purity detection, supplemented by ICP-MS heavy metal full screening and GC solvent residue testing, fully complying with international pharmaceutical and food-grade safety standards.
We support flexible supply modes covering small-batch research samples and large-scale industrial bulk orders, with customizable packaging solutions. Equipped with professional cold-chain logistics systems, we provide full-process temperature-controlled transportation and complete cold-chain documents. All products support independent batch traceability, with official COA and third-party test reports provided to help customers smoothly pass global regulatory audits and market declarations.
Source & Traceability
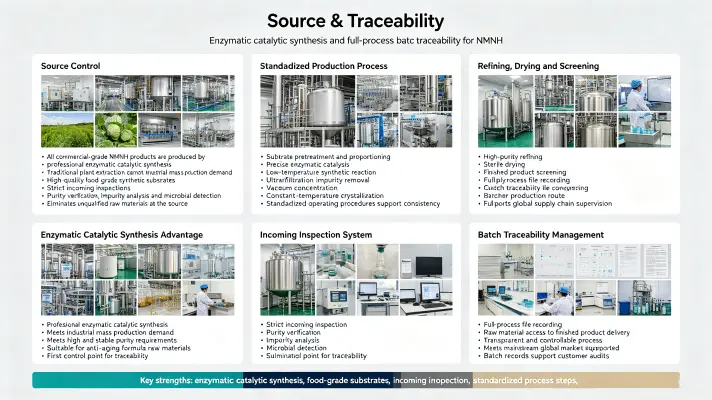
All commercial-grade NMNH products are produced by professional enzymatic catalytic synthesis. Traditional plant extraction technology cannot meet the industrial mass production demand and high and stable purity requirements of anti-aging formula raw materials. We exclusively adopt high-quality food-grade synthetic substrates, with strict incoming inspections including purity verification, impurity analysis and microbial detection to eliminate unqualified raw materials at the source.
The whole production process follows standardized operating procedures: substrate pretreatment and proportioning → precise enzymatic catalysis → low-temperature synthetic reaction → ultrafiltration impurity removal → vacuum concentration → constant-temperature crystallization → high-purity refining → sterile drying → finished product screening. We implement full-process file recording and batch traceability management, realizing full transparency and controllability from raw material access to finished product delivery, and fully meeting the supply chain supervision requirements of mainstream global markets.
Solubility & Stability Characteristics
Dissolution Properties
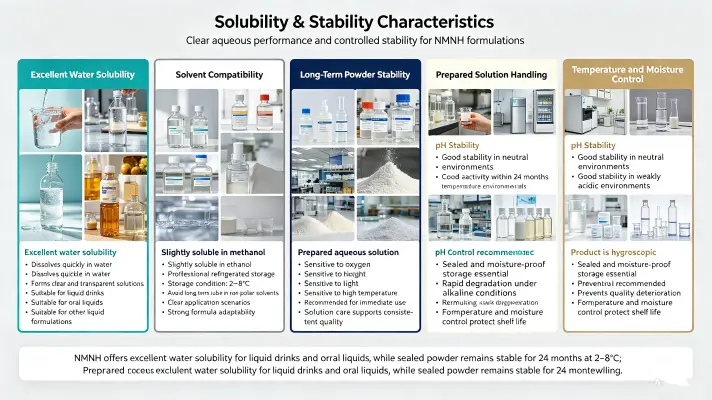
This raw material has excellent water solubility, which can be quickly dissolved in water to form clear and transparent solutions, perfectly suitable for liquid drinks, oral liquids and other liquid formulations. It is slightly soluble in methanol and ethanol solvents, and completely insoluble in oil-based raw materials and non-polar solvents, with clear application scenarios and strong formula adaptability.
Stability Profile
The sealed solid powder can maintain stable activity within 24 months under professional refrigerated storage conditions (2–8°C). Long-term room temperature placement will accelerate oxidative degradation and reduce product efficacy. The prepared aqueous solution is sensitive to oxygen, light and high temperature, so it is recommended to use it immediately after preparation. The product maintains good stability in neutral and weakly acidic environments, but it will degrade rapidly under alkaline conditions and high-temperature environments. In addition, the product is hygroscopic, so sealed and moisture-proof storage is essential to prevent powder agglomeration and quality deterioration.
Production Process
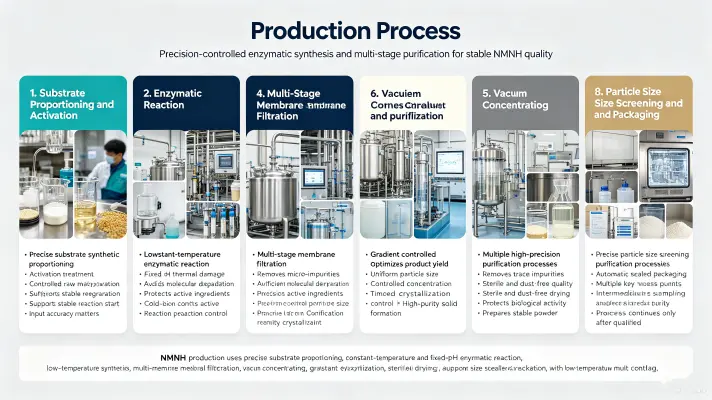
Our formal production process starts with precise substrate proportioning and activation treatment, followed by constant-temperature and fixed-pH enzymatic reaction to ensure sufficient and stable synthesis reaction. The low-temperature synthetic process effectively avoids thermal damage and molecular degradation of active ingredients, while multi-stage membrane filtration removes micro-impurities to reach pharmaceutical-grade purity standards.
After vacuum concentration to optimize product yield, we adopt gradient controlled crystallization technology to ensure uniform particle size of finished powder. Multiple high-precision purification processes remove trace impurities, and the finished products are dried in sterile and dust-free equipment. Finally, precise particle size screening and automatic sealed packaging are completed.
We set multiple key quality control points in the whole process, including reaction temperature control (tolerance ±0.5°C), real-time pH adjustment, accurate filtration pore size and timed crystallization control. Intermediate sampling and testing are carried out in each link, and the process can only be continued after the indicators are qualified, so as to fundamentally guarantee the stability of finished product quality.
Quality Assurance
Our quality management system covers the whole life cycle of products. From raw material qualification review and incoming inspection to multi-point online testing in the production process, every link implements strict quality control. All finished batches will be 100% fully inspected before delivery, including HPLC purity detection, ICP-MS heavy metal analysis, microbial limit test and ICH Q3C standard solvent residue verification.
Each batch of products corresponds to an independent traceability code, which can query complete production records, workshop environmental monitoring data and equipment calibration certificates. We regularly cooperate with authoritative third-party laboratories to complete product re-inspection and calibration, ensuring the accuracy of internal test data and providing credible independent test reports for customer global market audit and registration.
Packaging & Delivery
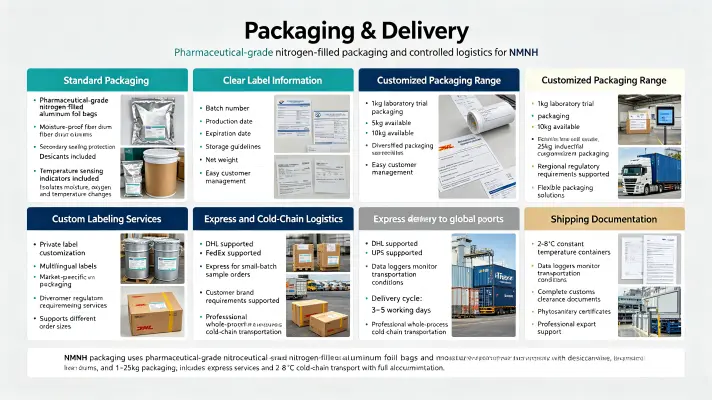
Our standard packaging adopts pharmaceutical-grade nitrogen-filled aluminum foil bags, which are placed in moisture-proof fiber drums for secondary sealing protection. Each package is equipped with desiccants and temperature sensing indicators to effectively isolate moisture, oxygen and temperature changes, and fully protect product activity. The packaging label clearly marks batch number, production date, expiration date, storage guidelines and net weight for easy customer management.
We provide diversified customized packaging services, covering 1kg laboratory trial packaging to 25kg industrial large-drum packaging. Private label customization, multilingual labels and market-specific customized packaging can be provided according to customer brand and regional regulatory requirements.
In terms of logistics, we support DHL, FedEx, UPS and other express services for small-batch sample orders, with a delivery cycle of 3-5 working days. Bulk industrial orders adopt professional whole-process cold-chain transportation, with 2-8°C constant temperature containers and data loggers to monitor transportation conditions in real time. All shipments are equipped with complete customs clearance documents and phytosanitary certificates to ensure smooth delivery to global ports.
Frequently Asked Questions
Q1: How fast can NMNH boost NAD+ levels compared with traditional precursors?
A1: With no complex metabolic conversion required, the product can significantly increase human NAD+ levels within 2-4 hours after administration, reaching peak efficacy faster and featuring higher bioavailability than conventional raw materials.
Q2: What is your minimum order quantity?
A2: We support 1kg small-batch trial orders for laboratory research and formula testing, with sufficient in-stock supply for immediate delivery. Large orders over 100kg are eligible for exclusive bulk discount and customized delivery schedule.
Q3: Can you provide complete regulatory supporting documents?
A3: Yes. Each batch is equipped with official COA, complete production records, stability test data and heavy metal detection reports. We can also provide targeted registration documents according to customers’ regional market demands.
Q4: What is the difference between 98% and 99% purity grades?
A4: 98% purity is cost-effective for conventional compound formulas and mass commercial products; 99% high-purity grade is suitable for premium health products, scientific research projects and high-standard export markets.
Q5: How to guarantee product stability during long-distance transportation?
A5: We adopt nitrogen-filled sealed packaging + cold-chain constant temperature transportation, equipped with temperature data loggers for whole-process monitoring, which effectively avoids oxidation and moisture absorption to ensure consistent product quality upon arrival.
Contact Us
If you have any demands for NMNH technical consultation, sample testing, formula customization and bulk order quotation, please feel free to contact our professional customer service and technical team via information@sxrebecca.com. We provide one-stop raw material solutions and professional technical support to help you develop competitive high-end anti-aging products.